Image of the day

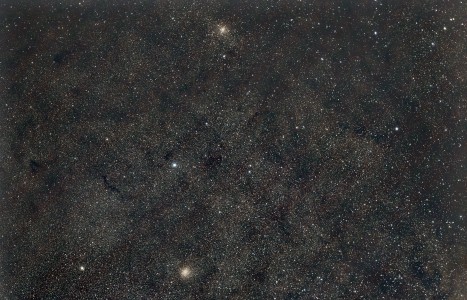
Captured by
Michael Scherman

Dual Clusters near Antares

My Account

New to Astromart?

Register an account...

Need Help?

Mass Production of High End Optics

Started by spaceflight, 05/25/2005 09:34PM
Posted 05/25/2005 09:34PM | Edited 05/25/2005 09:36PM Opening Post
Why cant computer controlled CNC type machines and/or tuned lasers be used to cut, ablate and figure very high quality optics? Wouldnt the repeatable precision of this type technology be more consistant, cheaper and faster then the some of the techniques used today (perhaps companies like Meade and Celestron are already employing?)

Scott

URL http://www.SPACEAHOLIC.com/

Preserving Space History for the Future
Posted 05/25/2005 09:41PM #1
Maybe someday. True figuring is still in the hands of 'opticians' literally.
Posted 05/25/2005 10:44PM #2
Why cant computer controlled CNC type machines and/or tuned lasers be used to cut, ablate and figure very high quality optics? Wouldnt the repeatable precision of this type technology be more consistant, cheaper and faster then the some of the techniques used today (perhaps companies like Meade and Celestron are already employing?)
------------------

Check out www.astro-physics.com Roland has a nice discussion of the fancy machines he uses. At the end of the fancy production line is Roland, he's the one that makes it happen.

jon
Posted 05/26/2005 06:51AM #3
Hello:
CNC machines are used for ion milling, which is used to touch up the figure of large optics. This uses a beam of charged particles to basically sandblast the optic on the atomic level. Only very small amounts of glass can be removed, so this is only used after traditional polishing. This is also quite expensive, and can't be used on some of the substrates not being used, such as silicon carbide. Large telescope optics (such as for Subaru and VLT) are made using computer controlled polishing machines. I suppose these can be adopted for amateur sized optics, and I wouldn't at all be surprised if folks like Meade and Celestron use such machines. With hand figured optics, there's a person who personally cares about how the optic come out, and will retest and refigure it until it's right. This is something a machine will never do.

Cheers
Mike Connelley
Posted 06/01/2005 10:25PM #4
>>Why cant computer controlled CNC type machines and/or tuned lasers be used to cut, ablate and figure very high quality optics>>

Lasers can't remove glass while still maintaining a polished surface. The whole idea of an optic is to be able to look through it, therefore the surface must be highly polished.

CNC machines, and even manual machines exist that can quickly polish a ground surface so you can look through it. In fact, the Criterion/B&L Schmidt-Cass corrector plates were polished at such high speeds that it took only 17 seconds to polish out a full 8" corrector. The plates came off the polishing machine smoking hot and would burn your finger. Accuracy was not the goal here, cost and production rate were the primary goal. One of our employees has one of these beauties. Talk about a rippled surface!

The act of polishing a piece of optical glass generates localized heat, only part of which is carried away by the recirculating slurry. The faster you polish, the more heat builds up. The underlying glass surface distorts with this heat, and when it cools, it springs back to a new surface figure, one that you may or may not want. A 6" lens that is polished quickly in 5 minutes or less from a fine ground surface may change as much as 10 - 30 waves. Even one that is polished in 1 - 2 hours at a slower pace will change at least 2 waves once off the polisher. Since a precision lens surface needs to be on the order of 1/10 wave, it follows that a super slow polishing process is needed at some point to achieve the final lens surface figure. Slow = time = money

The alternative to this is to polish a surface quickly, then measure it interferometrically, then use a magnetorheological finishing process (very expensive CNC machine) to place the final surface figure onto the lens. Measuring a surface requires at least 15-20 minutes of waiting time after handling a lens, and careful measurement by a qualified technician. Again, Slow + trained Tech = time = more money. On top of that, a magnetorheological finishing process is quite a long process also, and does require several intermediate measuring steps to achieve the best result. The end result is probably a 6" surface which costs on the order of $1000 of shop time production rate. Since at least 4 surfaces are required for a doublet, and 6 for a triplet, the cost can rise very quickly, even with the fanciest CNC equipment.

Right now there are no mechanical technologies that can achieve the highest accuracies that astronomical optics require at reasonable cost. Low cost is achieved by limiting something in the design or performance of the final optic.

Roland Christen